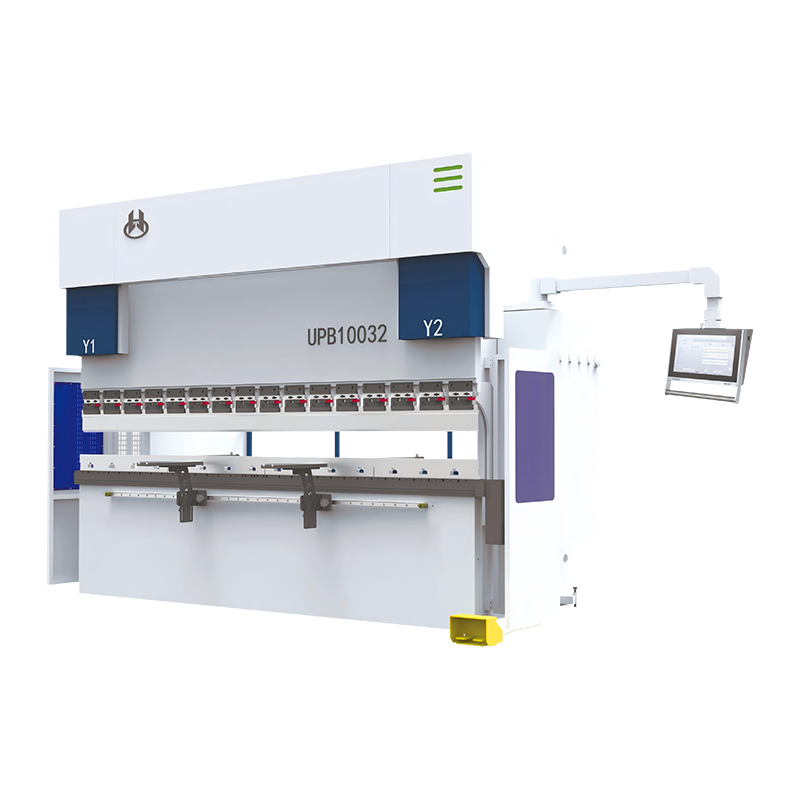
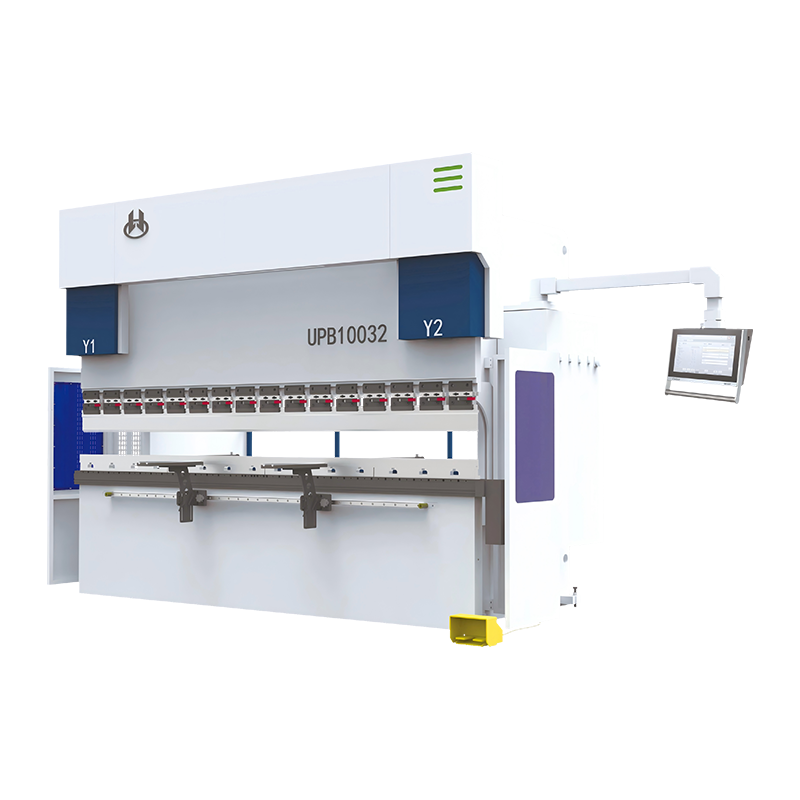
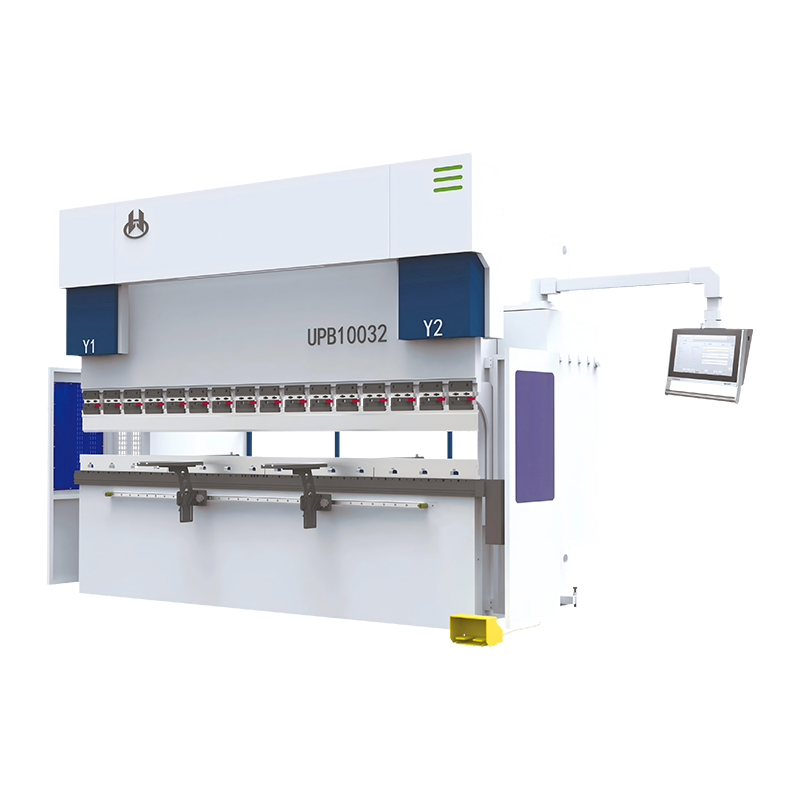
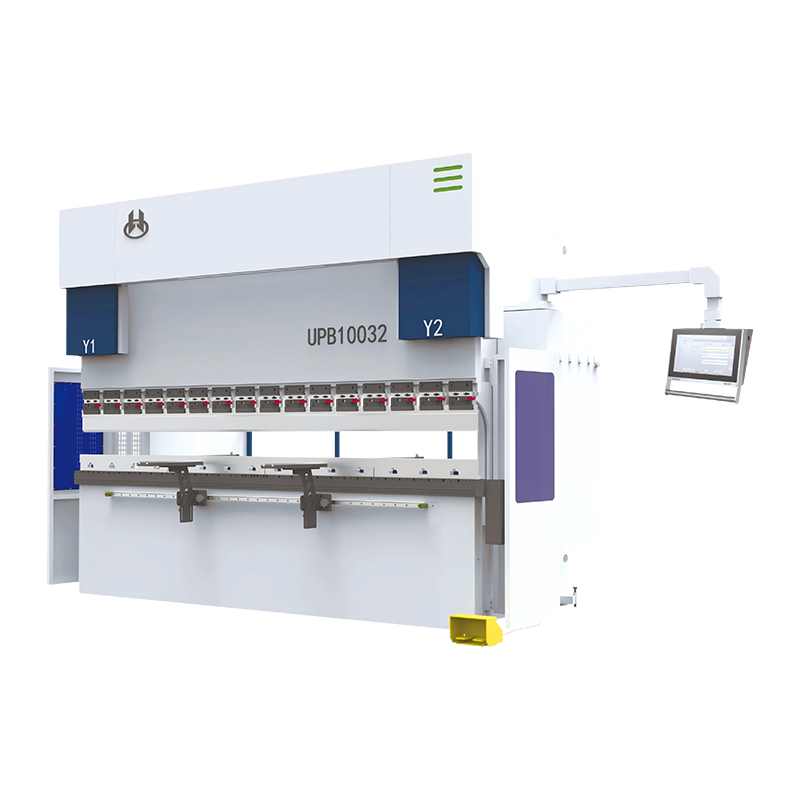
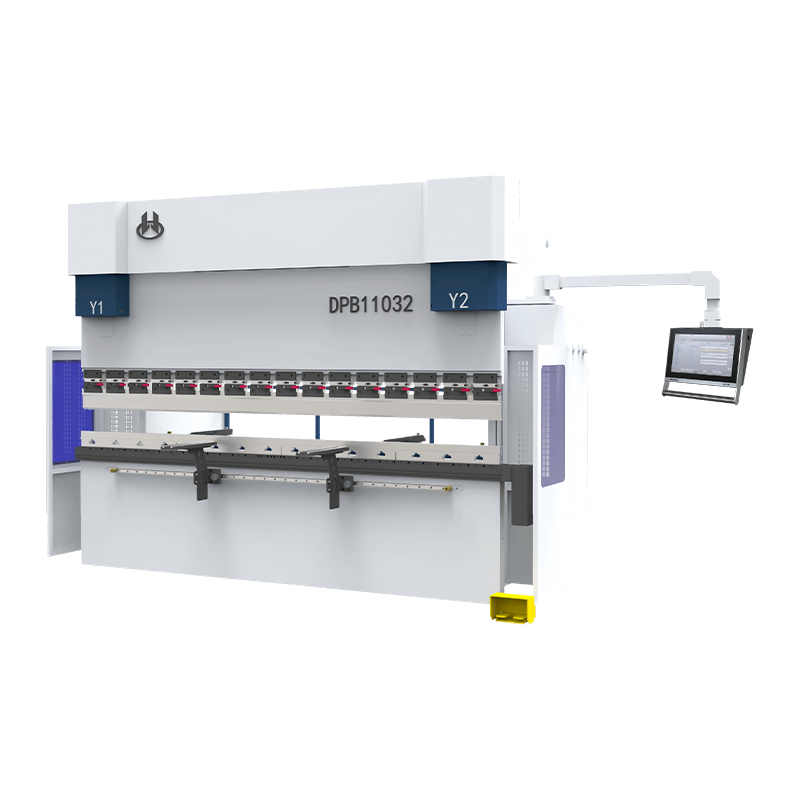
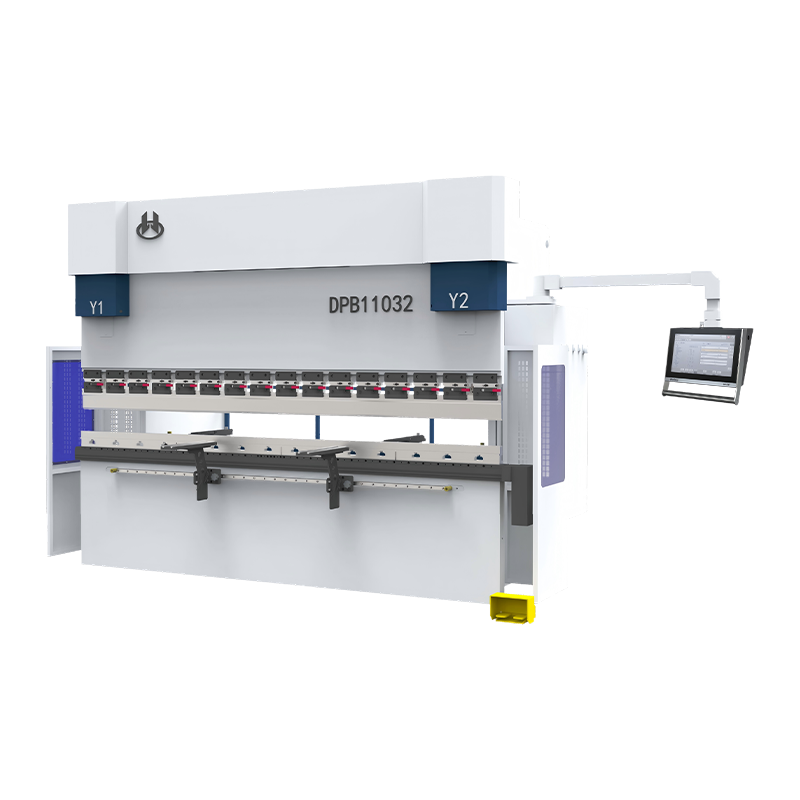
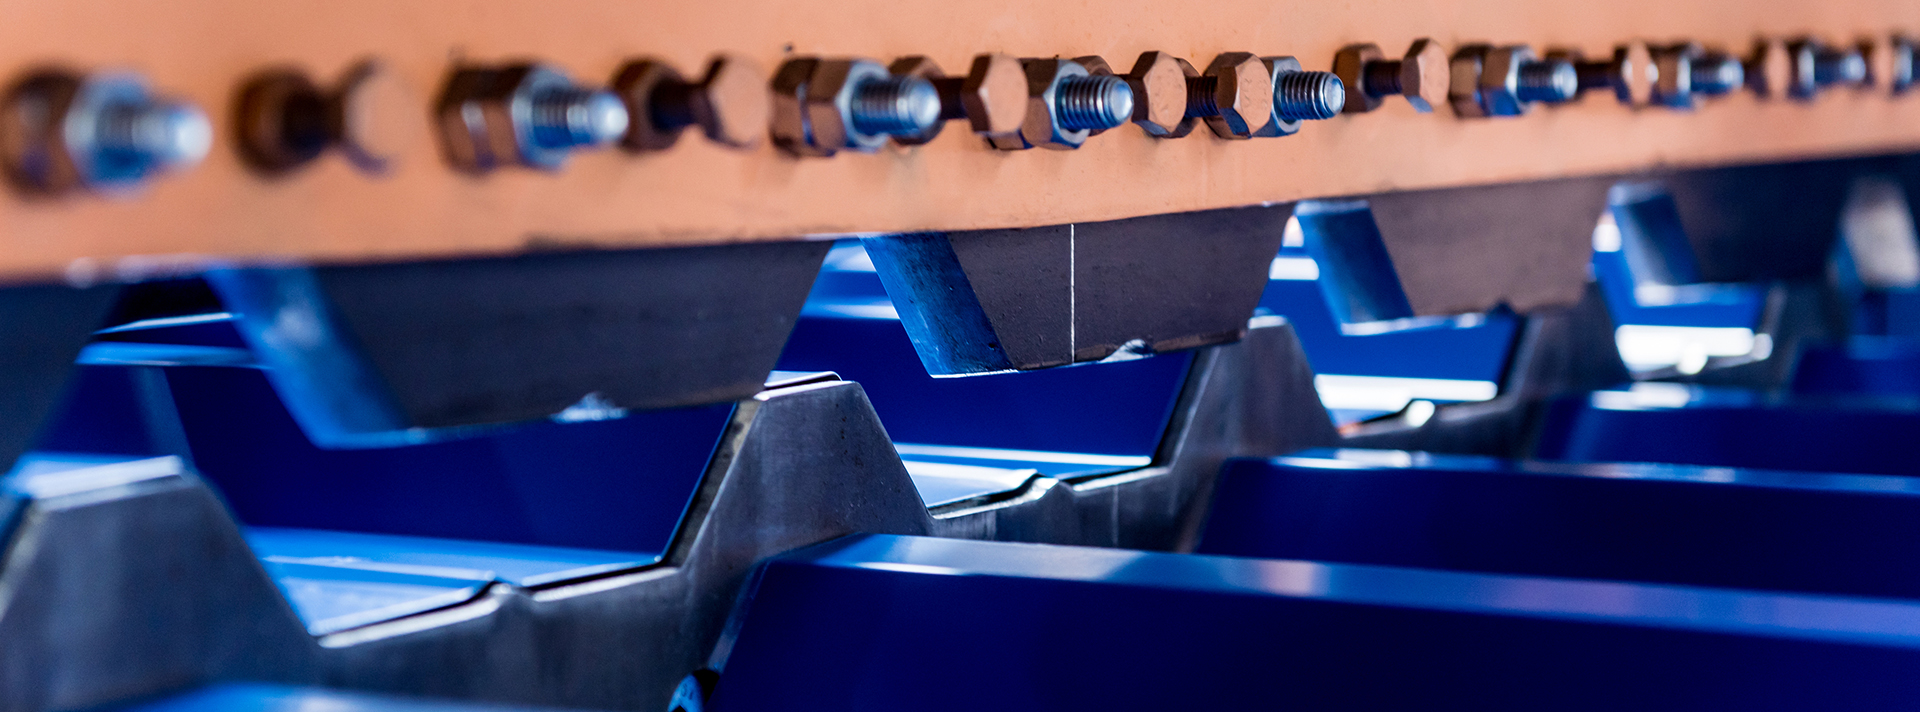
In bottom bending, the punch presses the sheet completely into the lower die so that the material closely follows the punch and die geometry. The final profile is therefore determined more directly by the tooling.
Compared with air bending, bottom bending normally requires higher forming force and more closely matched tools. The increased pressure helps stabilize the angle and reduce material springback.




 English